How to Choose a Low Pressure Injection Molding Machine?
Choosing a low pressure injection molding machine starts with the part, not the machine brochure. This process is often used to encapsulate delicate electronics, connectors, and small assemblies. A compact control module, for example, may need protection without the heat and pressure of conventional molding. The right equipment must match that real production need.
Start by checking the material’s processing window, required shot volume, mold size, and expected cycle time. Confirm that the machine’s pressure range suits the material and part geometry. Ask how accurately it controls temperature and pressure during each shot. Small variations can affect coverage, bonding, or the appearance of a finished edge. Measure sample parts. Inspect the results closely.
The machine should also fit your workflow. Consider loading access, changeover time, operator training, maintenance, and available technical support. Request clear specifications and, where possible, a trial using your own components and mold. A supplier’s example may not reflect your assembly. That matters. Compare the quoted capacity with your actual production plan, rather than choosing the largest model by default.
There is no perfect checklist. I would still question any recommendation that lacks test data or a clear explanation of its limits. A lower purchase price may look attractive, yet service delays or poor process control can cost more over time. The best choice is a low pressure injection molding machine that produces consistent parts, protects sensitive components, and leaves room for realistic future needs.
Understand the Low-Pressure Molding Process and Its Applications
How to Choose a Low Pressure Injection Molding Machine?
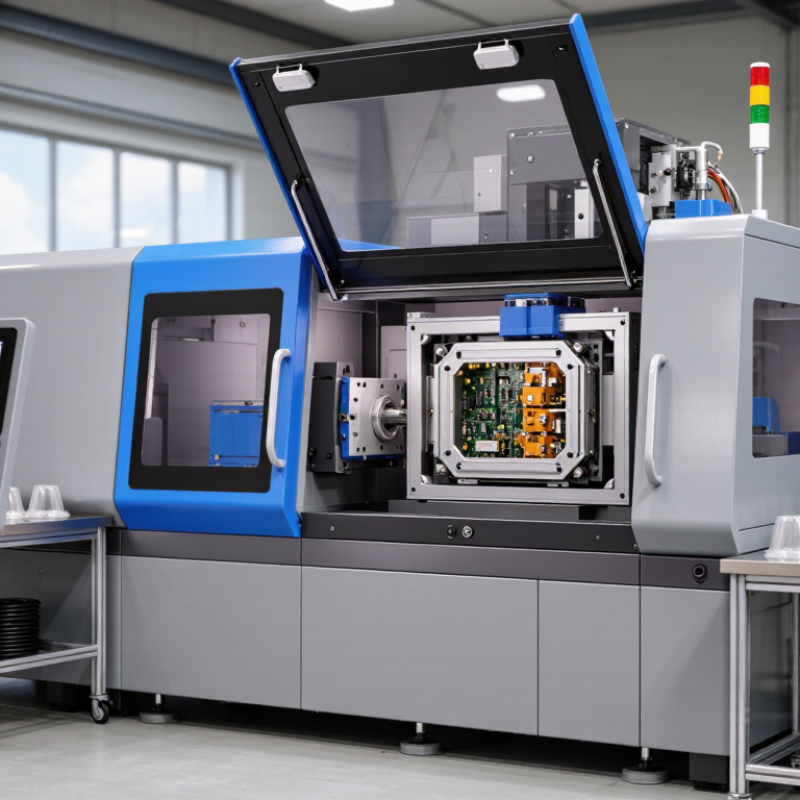
Low-pressure molding encapsulates components with a heated thermoplastic adhesive, injected gently into a simple mold. The material cools around wires, connectors, sensors, or circuit boards, forming a protective seal. This can reduce mechanical stress on delicate parts compared with conventional high-pressure molding. It is useful for electronics exposed to vibration, moisture, or repeated handling. The details matter.
The International Energy Agency’s Global EV Outlook 2024 reports nearly 14 million electric cars sold in 2023, about 18% of global car sales. That growth adds context for protective molding around vehicle wiring and electronic modules; it does not prove every part needs it. When comparing machines, check melt temperature, shot size, pressure control, and compatibility with the chosen material and component. A large clamp force is not automatically better. Ask for a trial using your actual connector or assembly, then inspect for voids, incomplete coverage, and heat damage. One detail is easy to miss: a process that seals beautifully can still make later repairs difficult. That trade-off deserves a real test.
Define Product, Material, and Production Requirements
Begin with the part, not the machine. Record its length, wall thickness, cavities, and sensitive features, such as exposed contacts or narrow sealing grooves. Note where the material must flow and where excess heat could damage components. Small details matter. A housing with dense connectors may need a different mold layout and shot size than a simple cap, even when both parts look similar.
Then define the material. Check its technical data sheet for melt temperature, viscosity, moisture sensitivity, and compatibility with the enclosed components. PlasticsEurope’s Plastics – the Fast Facts 2023 reports 400.3 million tonnes of plastics produced worldwide in 2022. That broad figure does not select a resin for you; it does show why “plastic” is too vague a specification. Confirm the exact grade and test it under realistic conditions. I would still question any plan based only on a resin’s name.
Production requirements turn those details into machine criteria. Estimate part and runner volume, target cycle time, daily output, and expected changeovers. Ask suppliers for usable shot volume and injection pressure at operating temperature, not just headline maximums. Also check mold dimensions, clamping capacity, and temperature control. A slow pilot run can hide trouble. Track cycle variation and scrap during a longer trial; the first sample may be misleading.
How to Choose a Low Pressure Injection Molding Machine?
Define product, material, and production requirements before comparing machine specifications.
Typical melt-temperature windows vary by material grade; confirm the exact range in the supplier’s technical data sheet. Check that the machine can maintain the required temperature, then match its shot capacity and injection pressure to the part’s geometry and material. Finally, size production capacity to the required cycle time and output.
Match Injection Capacity, Mold Size, and Operating Pressure
A low-pressure machine still needs enough usable shot capacity for the complete part and runner. Estimate the shot in grams, then check the machine’s rated capacity for the actual resin; different melt densities make a volume-only comparison unreliable. For example, a 48-gram part with a 7-gram runner needs about 55 grams per cycle. Keep the planned shot within the machine’s recommended processing range, not just below its maximum. Small margin. Real consequences. A barrel that is too large can increase residence time and risk material degradation.
Mold fit is more than platen dimensions. Check tie-bar spacing, mold thickness, daylight, opening stroke, and ejector travel against the tool drawing. A mold may fit the platen yet fail to open far enough to release a deep part. Operating pressure needs the same scrutiny: compare the required cavity-filling pressure with the machine’s available pressure at the intended flow rate. A maximum-pressure figure alone can mislead. PlasticsEurope’s Plastics – the Fast Facts 2024 reports 400.3 million tonnes of plastics production worldwide in 2022, spanning materials and applications with very different processing demands. That breadth is why a single “low-pressure” setting cannot define machine suitability. Check the resin datasheet and mold-flow assumptions; those inputs are not always perfect. Then validate the selected capacity and pressure with a controlled trial.
How to Choose a Low Pressure Injection Molding Machine? - Match Injection Capacity, Mold Size, and Operating Pressure
The figures below are representative selection examples, not universal machine specifications. Confirm the required shot weight, mold dimensions, material processing window, and pressure definitions with the machine supplier.
| Selection factor |
Compact setup |
General-purpose setup |
Large-part setup |
How to match it |
| Usable injection capacity |
Approx. 50–150 g per shot |
Approx. 150–500 g per shot |
Approx. 500–1,500 g per shot |
Compare the rated capacity with the total material needed for the part, runners, and any purge allowance. Avoid routinely operating at the extreme end of the rated range. |
| Example mold plan size |
About 200 × 150 mm |
About 350 × 300 mm |
About 500 × 400 mm |
Check the platen dimensions, tie-bar or frame clearance, mold locating features, and room for hoses and connectors. These example dimensions are not standard sizes. |
| Typical mold thickness to verify |
Approx. 100–250 mm |
Approx. 150–350 mm |
Approx. 200–450 mm |
Confirm the machine’s minimum and maximum mold height and available opening stroke against the actual mold drawing. |
| Representative clamping force |
Approx. 5–20 kN |
Approx. 20–50 kN |
Approx. 50–100 kN |
Use the lowest force that keeps the mold closed without flash under the intended process conditions. Required force depends on projected area, cavity layout, and material behavior. |
| Material injection pressure |
A low-pressure molding process may use approximately 0.5–5 MPa (5–50 bar) at the material, depending on material, temperature, flow path, and part geometry. |
Confirm whether the quoted pressure is material pressure at the nozzle, hydraulic pressure, or a maximum rating. These values are not interchangeable. |
| Mold opening and access |
Check part removal and operator access |
Check opening stroke and tool clearance |
Check handling space and lifting access |
Allow enough clearance for the part, sprue or feed system, fixtures, and safe loading or unloading. |
| Material and temperature control |
Verify material compatibility |
Verify melt stability and repeatability |
Verify heating capacity and cycle needs |
Match the heater, temperature range, and control accuracy to the material supplier’s processing recommendations. |
Selection check: Start with the required shot weight and mold drawing, then verify mold-height limits, opening stroke, clamping force, and material-side pressure. Run a process trial using the intended material and part geometry before finalizing the machine size.
Evaluate Controls, Compatibility, Safety, and Maintenance
A useful control system should make pressure, temperature, and cycle settings easy to read and adjust. Check whether it stores repeatable recipes and flags alarms clearly. Ask to see a sample setup, not just a feature list. Small screens can slow operators down.
Compatibility depends on your material, mold, and production needs. Confirm the machine’s shot capacity, clamping arrangement, temperature range, and connection requirements against your actual tooling. If possible, run a trial with the intended material and mold. This takes time, but assumptions can be costly. A trial may still miss changes caused by different operators or batches.
Inspect guards, emergency stops, interlocks, and pressure-release procedures before purchase. Low pressure does not mean no risk. Request a written maintenance schedule, then check whether seals, hoses, heaters, and filters are accessible for routine service. Easy access matters. I would not choose a machine on speed alone; a simpler model may be easier to maintain, though it could lack useful controls. That trade-off deserves a close look.
Compare Machine Costs, Supplier Support, and Long-Term Value
A low-pressure injection molding machine should be judged by more than its quoted price. Compare the complete setup: machine, compatible mold, material handling equipment, installation, operator training, and routine service. Ask for a written breakdown, not one bundled figure. A lower-cost unit may need extra tooling changes or longer setup time. Small costs add up.
Supplier support is part of the machine’s real cost. Before ordering, ask who handles commissioning, how quickly technicians usually respond, and whether remote troubleshooting is available. Request a maintenance schedule and prices for common wear parts.
Check the details. Manuals should explain pressure settings, material preparation, and safe shutdown clearly. If possible, run your own part during a trial and inspect fill consistency, cycle time, and surface quality. A polished demonstration is not enough.
Long-term value depends on predictable output and manageable upkeep, not the lowest number on a quotation. Estimate production hours, changeovers, energy use, and the cost of a delayed production day. Compare these assumptions across suppliers, then review them with your production team. No spreadsheet captures every surprise. Mark uncertain figures and verify them. A machine sized only for today’s volume may struggle when new molds arrive, while extra capacity can sit idle.