How to Set the Correct Mold Pressure for Injection Molding?
Mold pressure is not a number to copy from a machine manual. It is a process setting shaped by resin viscosity, part geometry, gate size, melt temperature, and tool condition. Set it too low, and a thin rib may short-shot. Set it too high, and flash can appear along the parting line. The right setting fills the cavity consistently without forcing the mold or masking another process problem.
The scale makes this control important. PlasticsEurope’s Plastics—the Fast Facts 2024 report estimates that global plastics production reached 413.8 million tonnes in 2023. That figure covers plastics broadly, not injection molding alone, but it shows the industrial reach of polymer processing. John Bozzelli, founder of Scientific Molding, Inc., is known for promoting a measured, data-led approach to molding. His practical principle can be stated simply: use process evidence, not guesswork, to guide pressure settings. Treat that as guidance, not a universal recipe.
In practice, start with the resin supplier’s processing guidance and the machine’s limits. Then review fill behavior, part weight, flash, and cavity-pressure data when available. A pressure value on the controller does not always equal pressure inside the cavity. Small changes matter. Record each adjustment, and change one variable at a time where possible. The honest complication is that pressure can compensate for poor temperature control or a restricted gate, at least temporarily. That may hide the cause. This guide explains how to choose a useful starting point, verify it on the press, and recognize when pressure is not the real problem.
Understanding Mold Pressure in Injection Molding
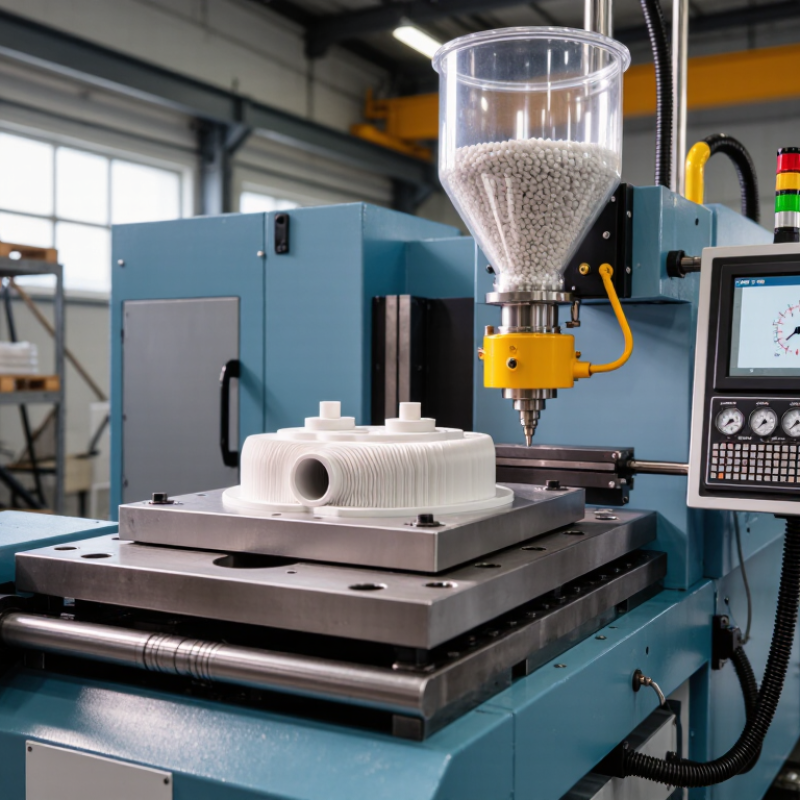
In injection molding, mold pressure generally refers to the pressure molten plastic exerts inside the cavity during filling and packing. It differs from the machine’s displayed injection pressure, measured upstream. Pressure drops as the material passes through the nozzle, runner, and gate. That distinction is easy to miss. A thin rib or a long flow path may receive much less pressure than the machine reading suggests.
Cavity pressure depends on resin viscosity, melt and mold temperatures, gate dimensions, part geometry, and fill speed. As plastic cools, it shrinks, so packing pressure helps feed material into the cavity before the gate freezes. Too little pressure can cause sink marks, voids, or incomplete details. Too much may create flash, residual stress, or difficult ejection. Small details matter.
A cavity-pressure sensor can show how pressure builds at a specific point, though one sensor cannot describe every area of a part. Without sensors, compare short-shot results, part weight, dimensions, and visible defects; these are useful but indirect clues. Adjust the transfer point and hold pressure in small steps, changing one variable at a time. Record each trial. A smooth-looking part can still contain stress, and a stable setting may shift when material or temperature changes. Process control is rarely perfectly tidy.
Identifying the Factors That Affect Required Pressure
How to Set the Correct Mold Pressure for Injection Molding?
Identifying the Factors That Affect Required Pressure
Required pressure depends on how easily the melt travels through the part, not on a single machine setting. Rosato’s Injection Molding Handbook gives a broad conventional injection-pressure range of roughly 70–140 MPa; the right value varies with resin, mold, and process. Treat that range as a reference, not a target. ASTM D1238 melt-flow testing can help compare material flow, but it does not directly predict pressure inside a specific mold.
Long flow paths, thin walls, small gates, and sharp turns increase resistance. Higher melt viscosity does too, especially when resin temperature is low or material has degraded. A 0.8 mm rib fed through a narrow gate may need substantially more pressure than a short, thick section. Check the fill pattern. A pressure spike near the end of filling can signal a restrictive gate or premature cooling, not simply a need to raise the machine limit.
Use pressure traces and short-shot trials alongside the material supplier’s processing data. Record the actual peak pressure, cushion, melt temperature, and fill time for each trial. Hold pressure is a separate adjustment: too little can leave sink marks, while too much may cause flash or stress. I would not trust a setting copied from another mold, even with the same resin. Small differences matter.
How to Set the Correct Mold Pressure for Injection Molding?
Identifying the Factors That Affect Required Pressure
This simplified comparison holds material, melt temperature, flow length, and filling speed constant. For flow between parallel plates, pressure drop is approximately proportional to the inverse cube of wall thickness; the index is normalized to 100 at 2.0 mm. In real molding, melt viscosity, flow-path length, gate and runner restrictions, mold temperature, and filling speed also affect the pressure required. Use this model as a guide, not as a machine-setting recommendation.
Calculating an Initial Pressure Range for the Mold
To estimate an initial mold-pressure range, separate machine injection pressure from pressure inside the cavity. The displayed machine value includes losses through the barrel, nozzle, runner, and gate; it is not a direct cavity reading. Start with the resin supplier’s processing window and the machine’s pressure limits. For a new tool, treat that window as a starting reference, not a guaranteed target.
Tips: Use a cavity-pressure sensor when available; it gives the clearest evidence. Without one, begin near the lower end of the recommended range and mold short shots. Increase pressure in small, recorded steps until the flow front fills the part smoothly. Watch for flash, burn marks, and rising peak pressure. Stop and check venting or temperature before adding more pressure.
Estimate clamp demand separately: multiply the projected part-and-runner area by expected cavity pressure, then allow a suitable safety margin for the machine and mold. Confirm units before comparing values; mixing bar, MPa, and area units can distort the result badly. Record melt temperature, mold temperature, fill time, and transfer position with each trial. The first estimate may be wrong. That is normal, but unexplained pressure jumps deserve investigation.
Setting and Adjusting Pressure During Trial Molding
During trial molding, adjust pressure in small, recorded steps rather than chasing a perfect number. Begin with the material supplier’s processing range and a conservative machine pressure limit. Confirm melt temperature, mold temperature, and fill speed first; pressure readings can mislead when these settings drift. Keep the starting shot slightly short, then increase the fill until the cavity fills consistently. Small changes matter.
Watch the part and the machine response together. A pressure trace, if available, can show a sudden rise near the end of filling, while short shots reveal where flow stalls. Set the transfer point from injection to holding pressure before the cavity is overpacked. Then raise holding pressure gradually to reduce sink marks, checking for flash, sticking, or excessive part weight.
More pressure is not always better.
A tidy pressure chart can still hide poor venting or uneven cooling, so inspect the molded part and review the setup before changing pressure again. Record each adjustment, including the resulting fill time and part weight; trial notes are easy to overlook, but they make the next run more reliable.
Verifying Pressure Through Part Quality and Process Data
A pressure setting is only a starting point. Verify it against the molded part and the machine record. Watch for short shots, flash, sink marks, warped edges, and changing dimensions. Then compare those observations with cavity-pressure curves, fill time, screw cushion, and peak injection pressure across repeated cycles. A rising pressure peak with a shrinking cushion may signal a restricted gate or inconsistent material—not a need to raise pressure. Watch the trend.
Use a consistent sample plan. Measure critical dimensions and part weight over consecutive shots, and plot the results beside pressure data. ASTM D955 provides a standardized method for measuring molding shrinkage; ISO 20457 covers tolerances and acceptance conditions for molded plastic parts. These references help connect process records to measurable outcomes. Where customer requirements call for capability indices, track Cpk against the specified target; 1.33 is a common internal benchmark, not a universal acceptance rule. A stable trace can still hide a quality problem. I have seen operators trust the machine display too much.
Tips: Change one pressure variable at a time, keep material and mold temperature steady, and label each trial. Compare at least 30 consecutive shots when checking short-term variation; investigate outliers before widening the pressure window.
How to Set the Correct Mold Pressure for Injection Molding? - Verifying Pressure Through Part Quality and Process Data
Representative process-validation example for one molded part. Values are illustrative; acceptable pressure settings depend on the resin, part geometry, mold, and machine. Use cavity-pressure readings together with part inspection and stable process data.
| Trial |
Peak Injection Pressure
(MPa) |
Peak Cavity Pressure
(MPa) |
Hold Pressure
(MPa) |
Fill Time
(s) |
End-of-Hold Cushion
(mm) |
Part Weight
(g) |
Critical Dimension
(mm) |
Part Quality Observation |
Assessment |
| Trial A |
72 |
31 |
38 |
0.92 |
4.8 |
17.72 |
24.91 |
Short fill at the end of the flow path |
Reject — pressure too low for complete filling |
| Trial B |
82 |
38 |
44 |
0.86 |
4.2 |
17.91 |
24.97 |
Complete fill; no visible flash; measurements within limits |
Pass — acceptable, near lower process window |
| Trial C |
88 |
43 |
48 |
0.84 |
4.0 |
18.00 |
25.00 |
Complete fill; uniform appearance; stable part weight |
Pass — recommended starting condition |
| Trial D |
94 |
49 |
52 |
0.82 |
3.8 |
18.08 |
25.04 |
Complete fill; no visible flash; dimensions within limits |
Pass — upper part of the example process window |
| Trial E |
101 |
56 |
58 |
0.80 |
3.5 |
18.20 |
25.09 |
Flash at the parting line; part weight and dimension above limits |
Reject — excessive pressure and overpacking indicated |
| Trial F |
88 |
43 |
48 |
0.84 |
4.1 |
18.01 |
25.01 |
Repeat run; complete fill and measurements consistent with Trial C |
Pass — repeatability confirmed |
|
Example acceptance checks: part weight 17.90–18.10 g; critical dimension 24.95–25.05 mm; no short shots or visible flash. Confirm limits against the applicable part drawing and control plan.
|